How Do You Prove a Coil Package Passed the Test?
"The package looked good" is not a test result — it cannot be repeated, compared, or defended. This guide shows how to define samples, methods, and pass/fail rules that survive an audit and a shift change.
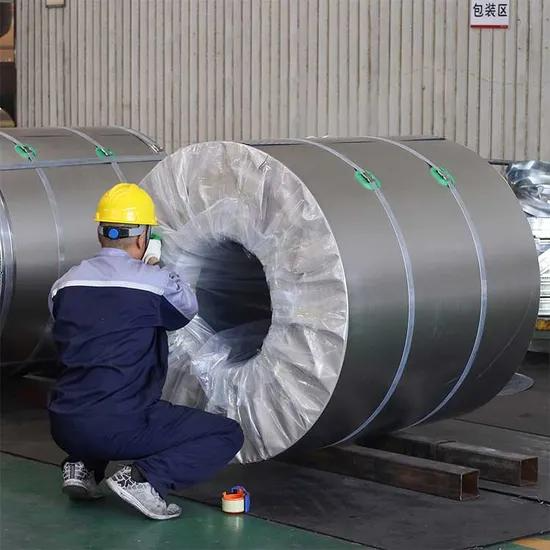
How to Run a Packaging Quality Test: Method, Samples and Acceptance
How to Run a Packaging Quality Test: Method, Samples and Acceptance
A packaging quality test is only useful when the method, sample, and acceptance criteria are defined before the test begins. A test that says "the package looked good" cannot be repeated, compared, or defended.
This guide helps quality, engineering, and operations teams design a repeatable packaging quality test for an automatic coil packing line. The goal is not a one-off inspection but a method the plant can run again for every product family.
Define the Test Objective First
State what the test must prove: coverage, overlap, tension, tail seal, edge protection, material usage, cycle time, or the condition after handling. A test that tries to prove everything at once usually proves nothing.
Write the acceptance criterion for each objective before the test. Keep the criteria specific enough that a different operator can apply them the same way.
The image shows an engineering team discussing a coil packaging line solution in a meeting room. This is where the test objective should be agreed before anyone touches the line: what the test must prove, who performs it, and who decides pass or fail.
Define the Sample
Select representative coils from the actual product mix: the most common, the narrowest, the widest, the heaviest, the lightest, and the most sensitive surface. Include coils that require a different recipe or orientation.
Record the measured dimensions, weight, surface condition, and material lot before the test.
| Sample factor | Why it matters |
|---|---|
| Most common coil | Reflects the daily load |
| Extreme width and weight | Proves the usable range of the line |
| Sensitive surface | Checks edge protection and contact points |
| Different recipe or orientation | Proves the changeover logic |
Define the Test Method
For each objective, state how it is measured:
- Coverage and overlap: measured on the wrapped surface at defined points.
- Tension or tightness: checked by a defined hand or tool method.
- Tail seal: checked after the coil is moved, not only while stationary.
- Material usage: measured as film length or weight per coil.
- Cycle time: measured from a defined start to a defined end.
Name the person who performs the measurement and the person who confirms the result. A method with no named owner cannot be repeated.

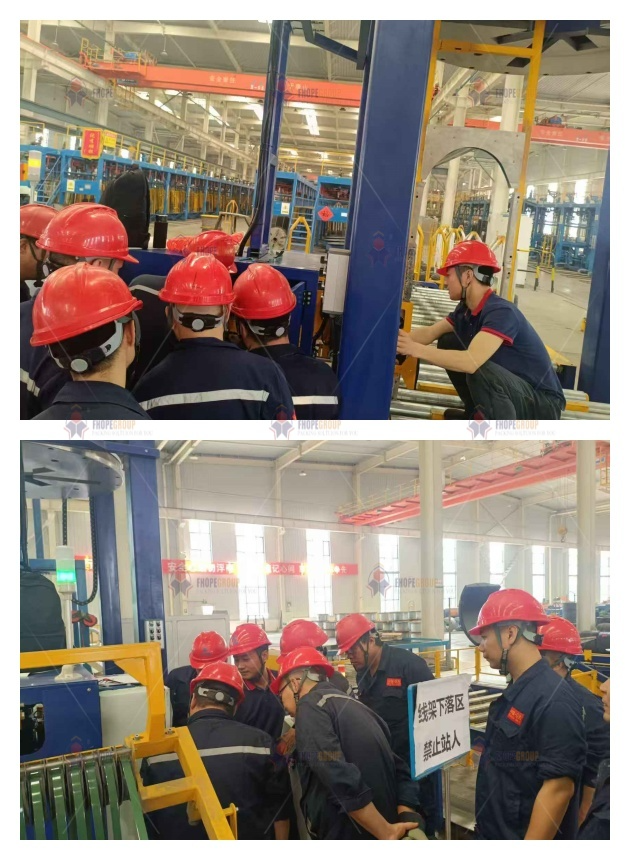
The image shows two people at a steel coil wrapping machine on the plant floor. The method should be fixed at the machine itself so the measured points, the operator action, and the confirmation step stay the same on every run.
Test Normal and Extreme Cases
Run the normal product first, then the extreme cases that matter for the line. Include at least one full cycle and one cycle with a material replenishment or an interruption, because recovery affects the finished package.
The test should also cover a changeover between two families.
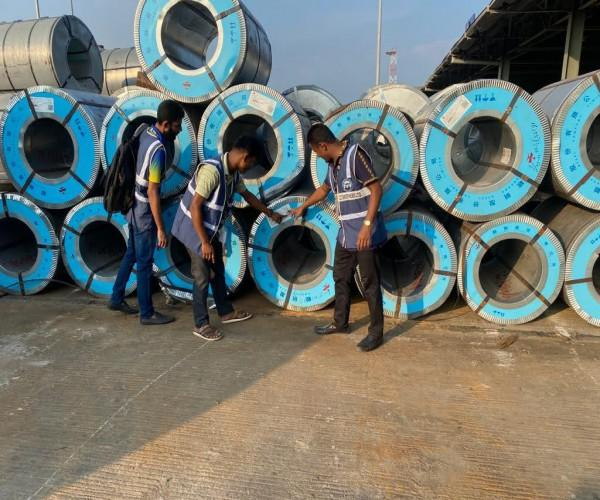
The image shows a team inspecting a steel coil package after unpacking. This is the point where the test becomes meaningful: the package has been handled and moved, and the condition of the coil and its protection can now be checked.
Record the Evidence
Take photos or videos of the package before and after movement, and record the measurements and the pass/fail result for each criterion. Keep the raw records, including failures.
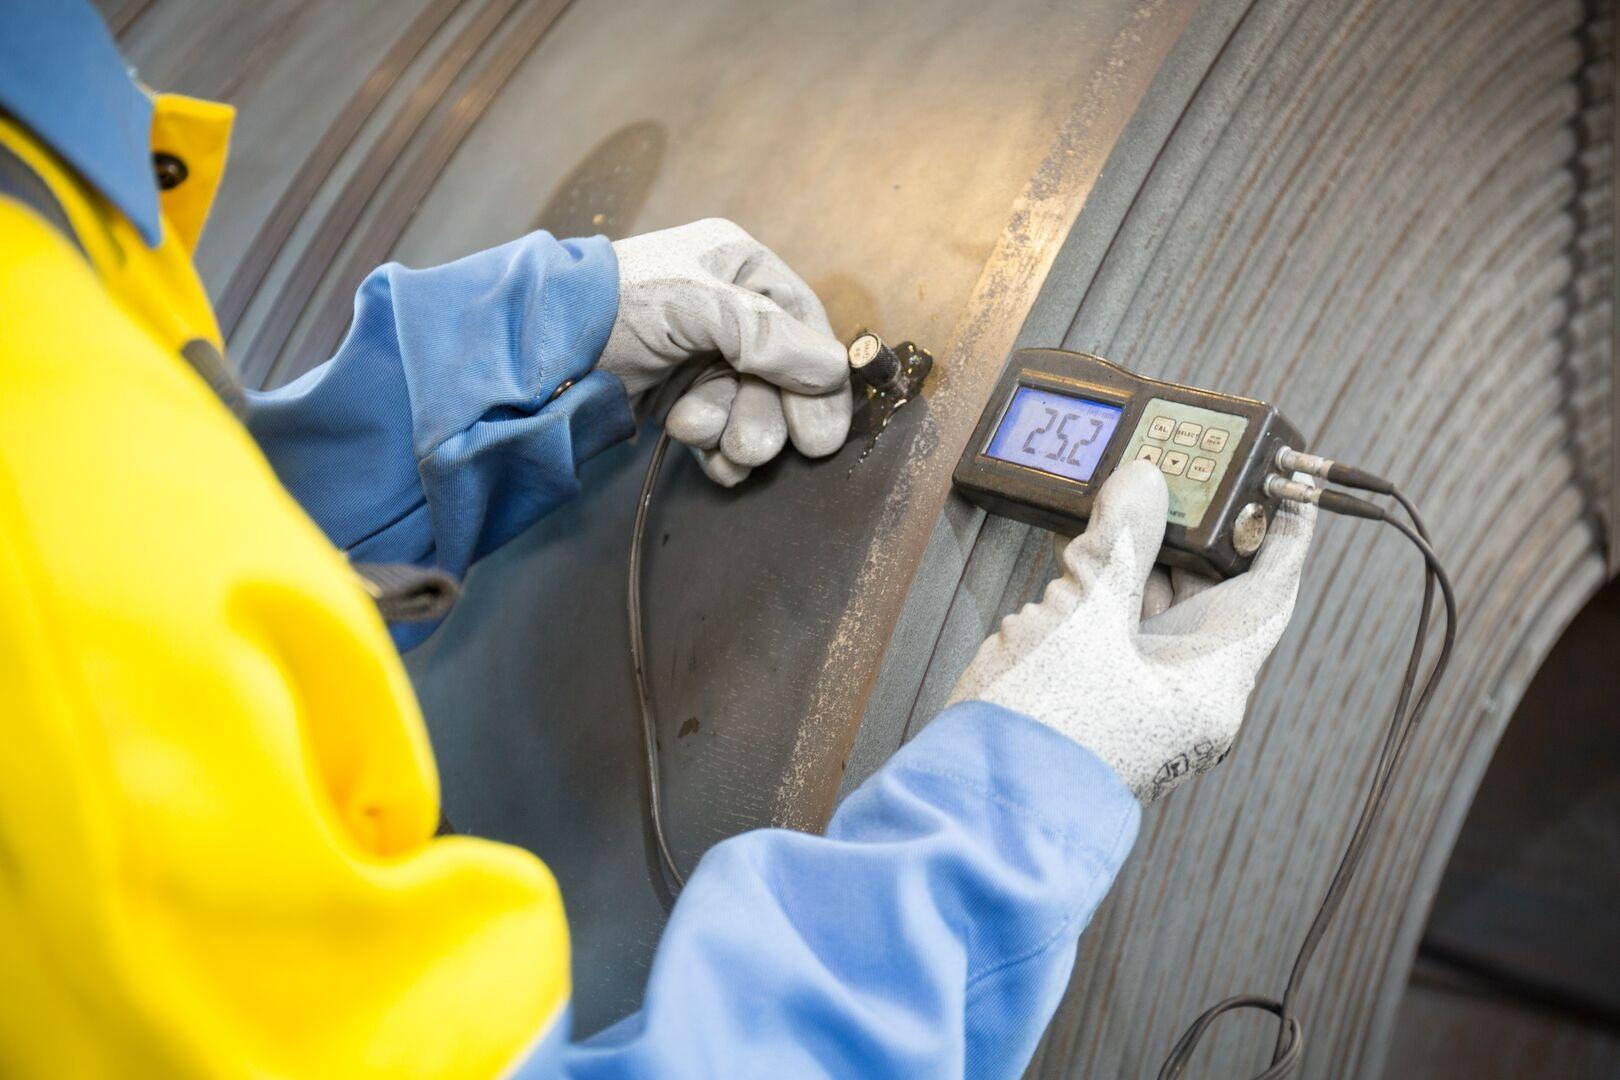
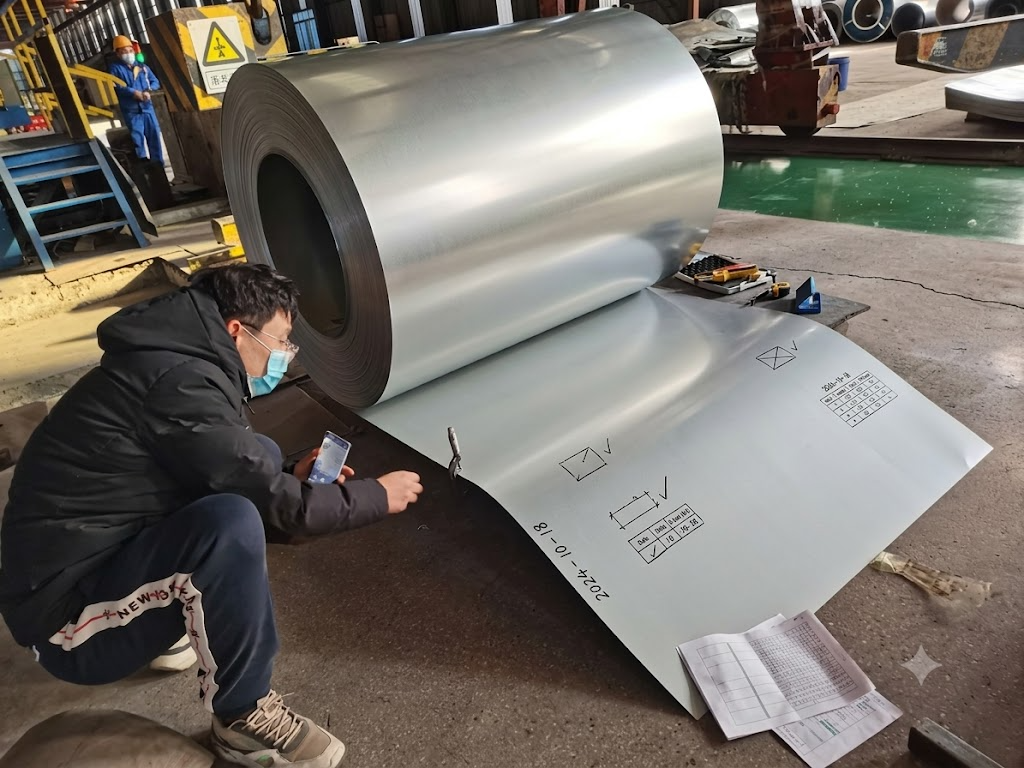
The image shows a closer inspection of an unpacked steel coil, with the surface checked for rust protection and damage after the transport packaging has been removed. This kind of visual record belongs in the test file because it documents the condition the package was meant to protect.
The evidence file should contain:
- the defined sample and its measured condition
- the method and the person who performed it
- photos or video before and after movement
- the pass/fail result for every criterion
- the failure record, including what was changed before retest
Watch the complete process of a fully automatic steel coil packaging line:

Define the Decision Rule
State how many failures cause a retest, a recipe change, or a machine adjustment. Do not change several parameters at once after a failure; change one, retest, and record the result.
| Result | Next action |
|---|---|
| All criteria pass | Record and keep the sample record |
| One criterion fails | Change one parameter, retest, record |
| Repeated failure | Treat as a recipe or machine adjustment, not a one-off event |
A Practical Next Step
Create a one-page quality test sheet with objective, sample, method, criterion, and result. Run it for each product family and keep the completed sheets as the packaging quality record for the automatic coil packing line.
Visual Details
Click to enlarge

Click to enlarge

Click to enlarge

Click to enlarge
Watch How It Works
Discover how our automated packaging solutions optimize your production line efficiency. This video demonstrates the seamless operation designed for maximum protection.
Trusted by Steel Mills & Industry Leaders
Global manufacturers rely on FHOPE heavy duty packaging equipment


Ready to optimize your packaging line?
Get a custom quote with ROI analysis. Our engineers respond within 24 hours.
- Free layout design
- Global installation support
- 2-year warranty included
Your information is secure and will never be shared.
Related Machines
Steel Coil Packaging line
View Details →
Vertical coil packaging line
View Details →
Hose Coil Packaging line
View Details →
Copper Coil Packaging line
View Details →
Wire Coil Packaging line
View Details →
Panel Packaging line
View Details →
Pipe Bagging Machine
View Details →
Aluminum profile packing line
View Details →
FHOPE Automatic pipe tube bundling&strapping line
View Details →
Automatic pipe tube bundling & strapping line
View Details →
Automatic steel tube strapping machine
View Details →
FHOPE Automatic steel tube packing machine
View Details →
Automatic plastic Pipe strapping packing line
View Details →
Automatic PPR/PVC Pipe bagging line
View Details →
Platsic pipe bag packing machine
View Details →
Tyre Packing Machine FPT-200
View Details →
Tyre Packing Machine FPT-300
View Details →
Tyre Packing Machine FPT-400
View Details →
Cable Coil Packing Machine-FPCA100
View Details →