Can Your New Packing Line Work with Existing Cranes?
Integrating a coil packing line with existing conveyors and cranes starts at the interface: receiving positions, transfer signals, buffers, and safety interlocks. Learn how to define every handoff before the line scope is fixed.

How to Integrate a Coil Packing Line with Existing Conveyors and Cranes
How to Integrate a Coil Packing Line with Existing Conveyors and Cranes
Most coil packing lines do not start from an empty floor. They are added to a production area that already has conveyors, crane access, forklift routes, and established material flow. The integration boundary is where the new line meets the existing equipment, and that boundary decides whether the project succeeds.
This guide helps project, engineering, and operations teams define the interface between a new automatic coil packing line and existing handling systems.
| Interface element | What must be defined |
|---|---|
| Receiving position | Location and coil orientation at every handoff |
| Transfer control | Who controls the transfer and what signal confirms readiness |
| Stop on either side | How each system waits, rejects, or recovers |
| Buffer | Capacity, full condition, and route when full |
| Safety interlock | Shared access zone and lockout-tagout boundary |
Map the Existing Flow Before the New Line
Record how coils arrive today: from a slitting line, a roller table, a walking beam, a crane, or a coil car. Mark the existing buffers, transfer points, and the people or systems that control each handoff.
The new line must fit into that flow without creating a new bottleneck or blocking the equipment it depends on.
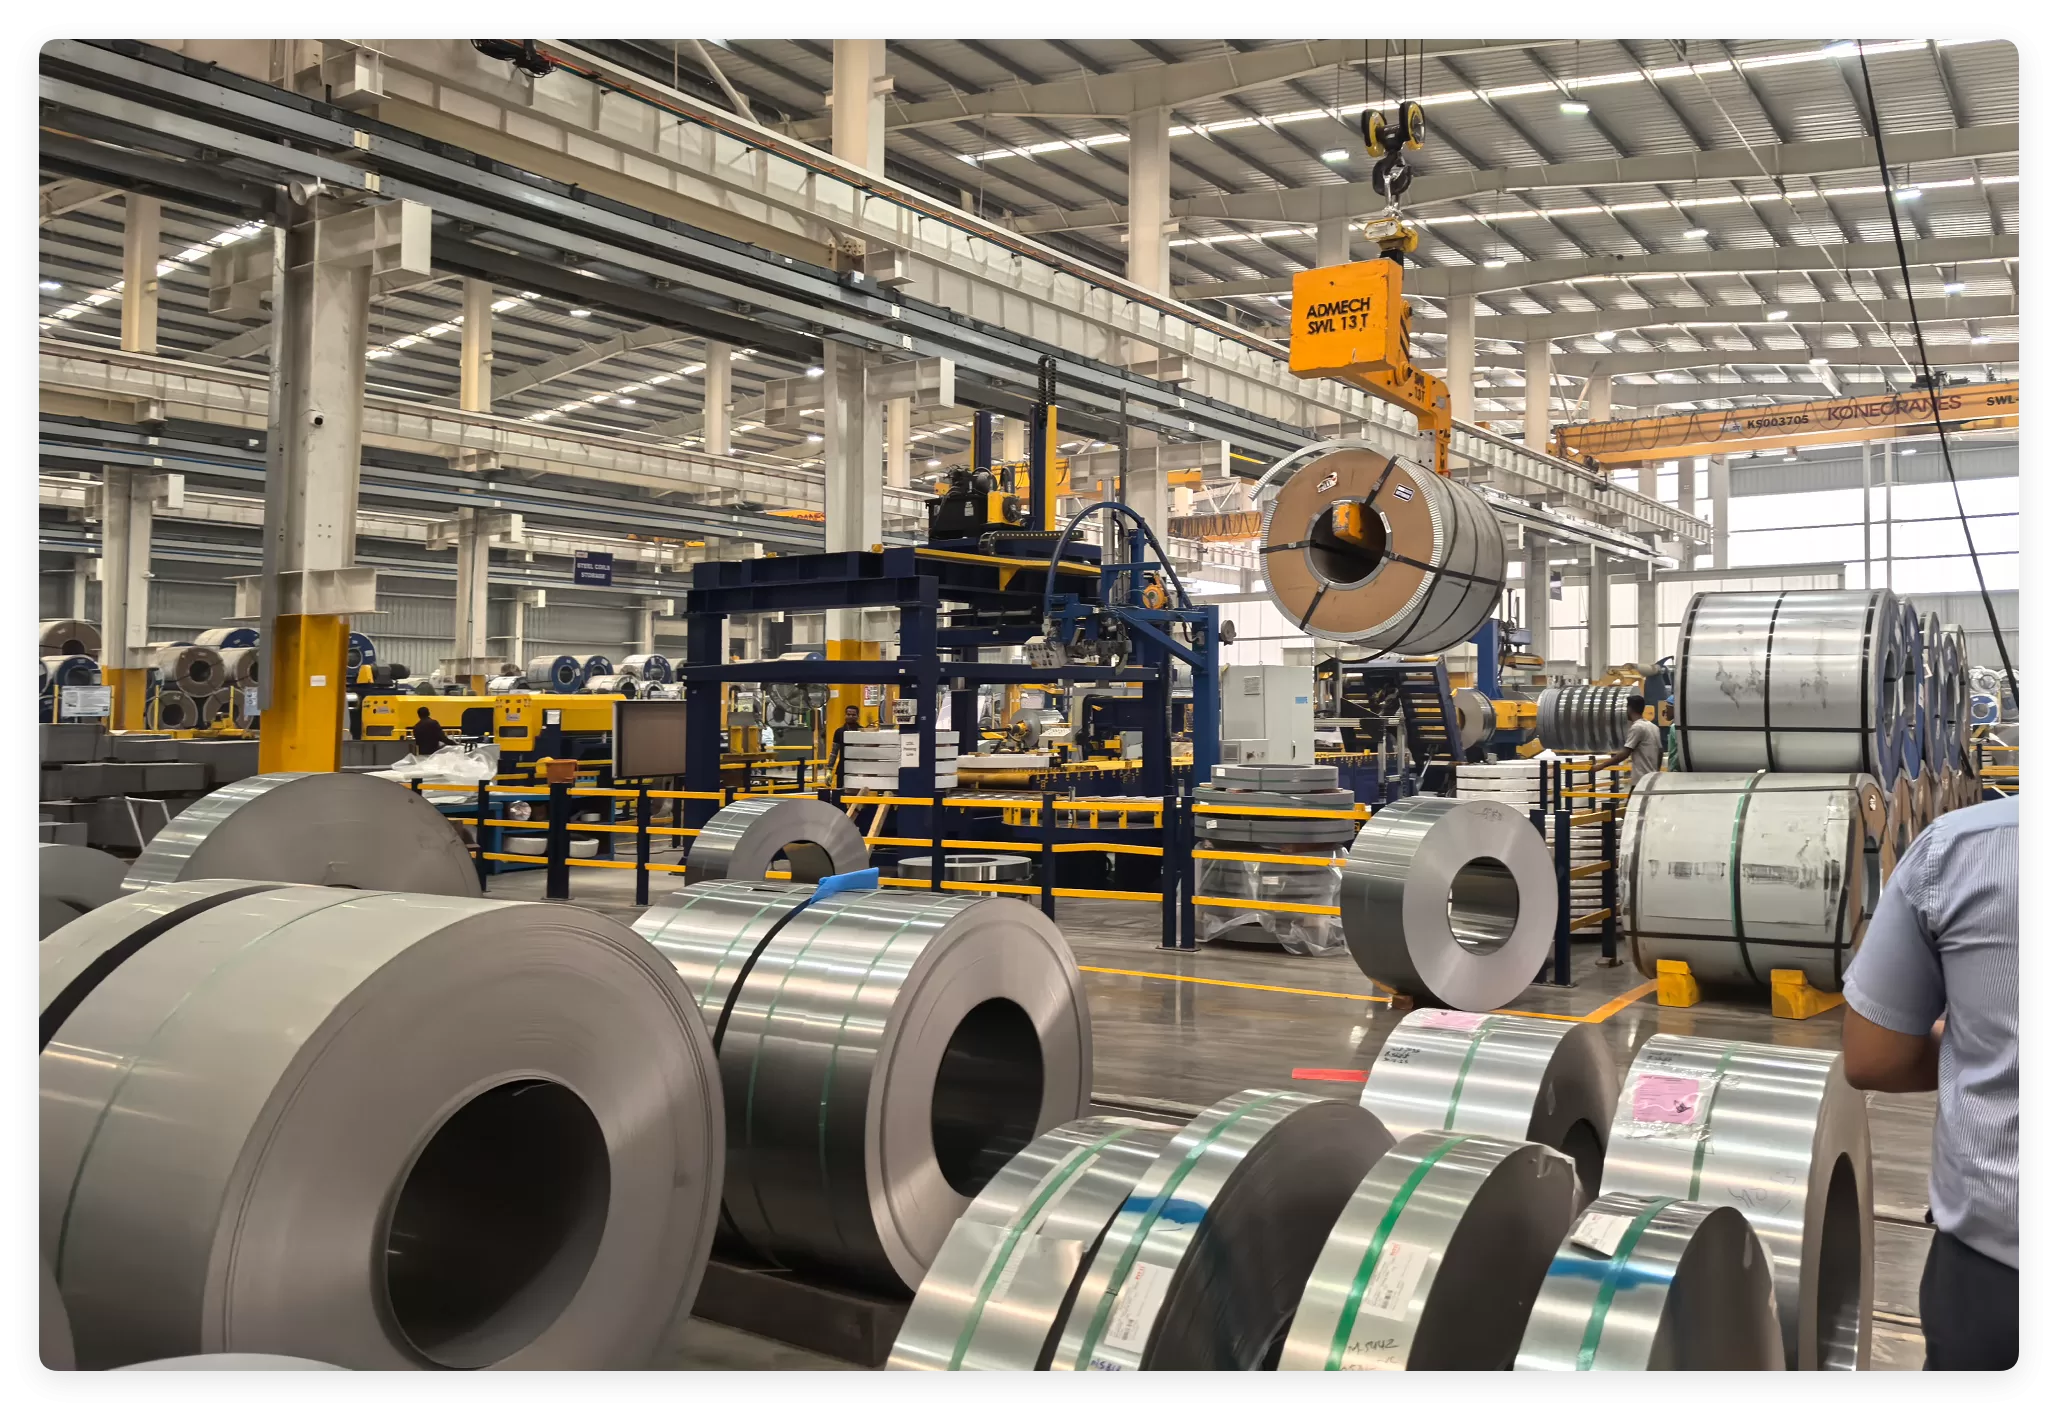
The image shows a steel service center coil packaging automation context. The new line must be mapped against the existing conveyors, crane routes, and material flow before any equipment position is fixed.
Define the Physical Interface
For every handoff, state:
- Where the coil is received and at what orientation.
- Who controls the transfer.
- What signal confirms the coil is ready.
- What happens when the new line is stopped.
- What happens when the existing equipment is stopped.
The interface is complete only when both sides can wait, reject, or recover without stopping the other in an unsafe way.
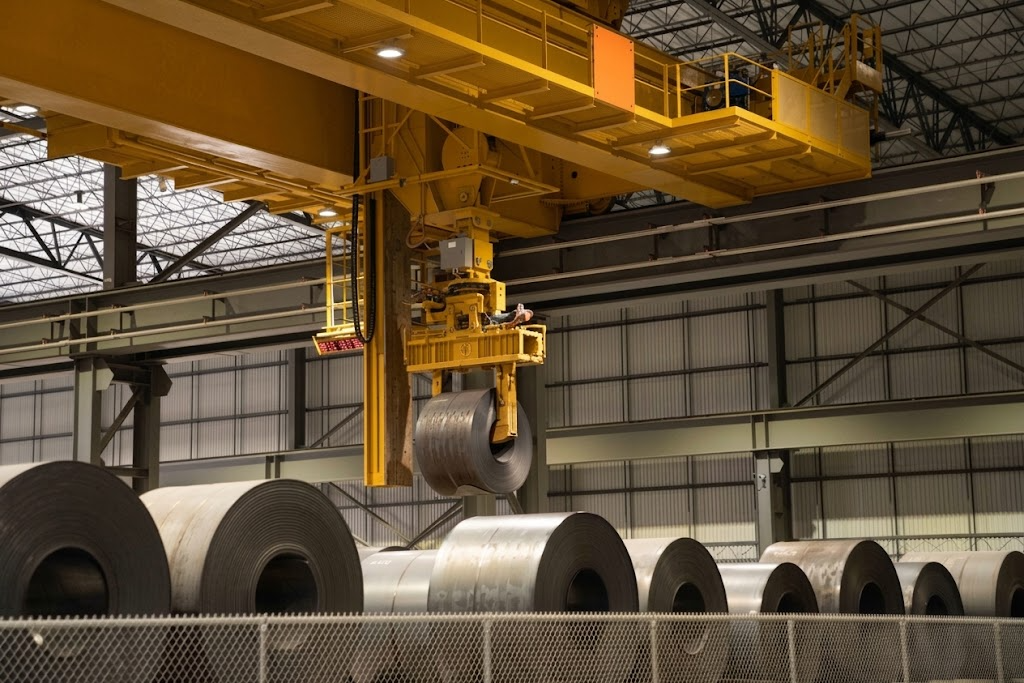
The image shows crane and handling integration. The crane landing position, the signal that the coil is placed correctly, and the route when the line cannot accept the coil must all be part of the interface.
Decide How the Coil Is Handed Over
A crane-loaded line needs a defined landing position, a safe approach, and a signal that the coil is placed correctly. A conveyor-fed line needs matched speed, height, and control signals between the existing conveyor and the new line.
Do not assume the crane or conveyor can simply "stop at the line." The interface must be tested with the actual control logic.
Add Buffering at the Boundary
The difference between upstream release and downstream cycle time should be absorbed by a defined buffer. Show the buffer capacity, the full condition, and the route when the buffer is full.
If the existing equipment is faster than the new line, the buffer is not a luxury; it is the system boundary.
Include Safety in the Interface
The new line's guarding and the existing crane or conveyor routes share the same space. Define the access zone, the interlock between moving equipment, and the lockout-tagout boundary for both systems.
An integration that ignores the shared area will create a risk that neither system owner can control.
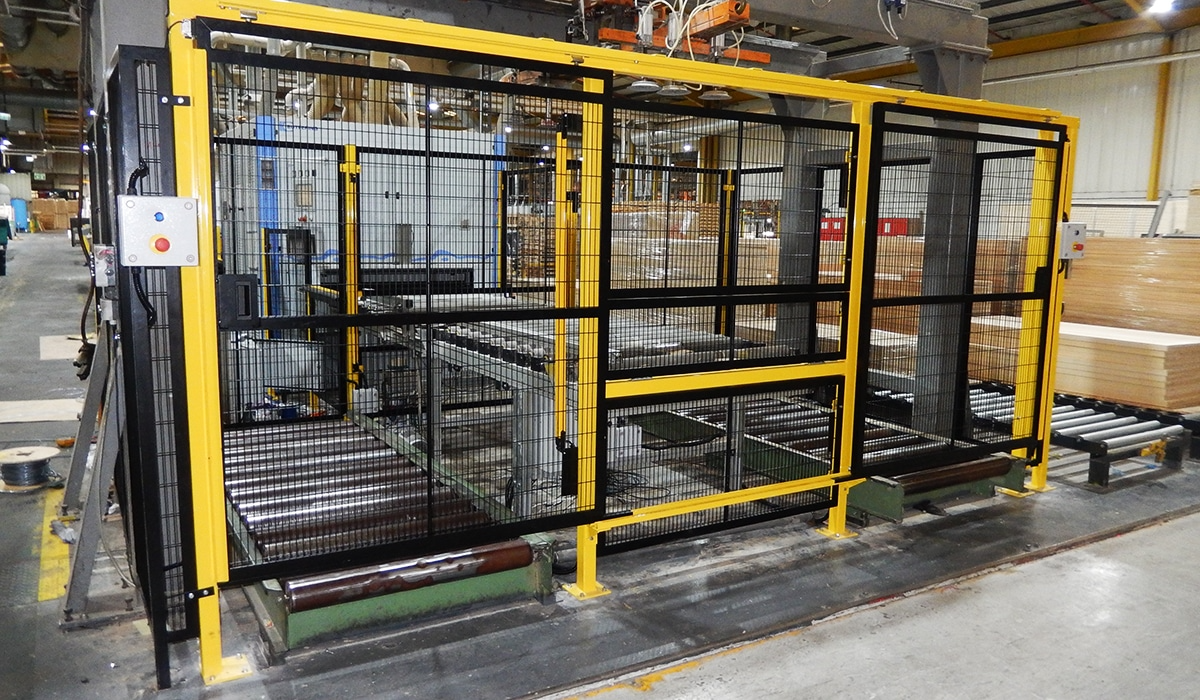
The image shows industrial safety interlocks and protective enclosures. The shared area between the existing handling system and the new line needs interlocks and a clear lockout-tagout boundary.
Test the Handoff During Acceptance
FAT/SAT should include a coil arriving from the existing conveyor or crane, a stop on either side, and a recovery. Record the signals, the waits, and the intervention required.

The image shows people working around a steel coil wrapping machine during its site-specific procedure. The handoff test should be run at the site, with the same operators, signals, and control logic that will be used in production.
A Practical Next Step
Draw the existing and new systems on one diagram with all handoffs, buffers, and interlocks. Review it with the owners of both systems before the line scope is fixed.
Keep the same interface diagram visible for the automatic coil packing line comparison and acceptance tests.
Watch an automatic steel coil packaging line in Malaysia with smart coil wrapping and strapping system:

Visual Details

Click to enlarge

Click to enlarge
Click to enlarge
Click to enlarge
Watch How It Works
Discover how our automated packaging solutions optimize your production line efficiency. This video demonstrates the seamless operation designed for maximum protection.
Trusted by Steel Mills & Industry Leaders
Global manufacturers rely on FHOPE heavy duty packaging equipment


Ready to optimize your packaging line?
Get a custom quote with ROI analysis. Our engineers respond within 24 hours.
- Free layout design
- Global installation support
- 2-year warranty included
Your information is secure and will never be shared.
Related Machines
Steel Coil Packaging line
View Details →
Vertical coil packaging line
View Details →
Hose Coil Packaging line
View Details →
Copper Coil Packaging line
View Details →
Wire Coil Packaging line
View Details →
Panel Packaging line
View Details →
Pipe Bagging Machine
View Details →
Aluminum profile packing line
View Details →
FHOPE Automatic pipe tube bundling&strapping line
View Details →
Automatic pipe tube bundling & strapping line
View Details →
Automatic steel tube strapping machine
View Details →
FHOPE Automatic steel tube packing machine
View Details →
Automatic plastic Pipe strapping packing line
View Details →
Automatic PPR/PVC Pipe bagging line
View Details →
Platsic pipe bag packing machine
View Details →
Tyre Packing Machine FPT-200
View Details →
Tyre Packing Machine FPT-300
View Details →
Tyre Packing Machine FPT-400
View Details →
Cable Coil Packing Machine-FPCA100
View Details →